Blow-Up Ratio (BUR): Formula & Effects on Film Quality
What Is the Blow-Up Ratio in Blown Film?
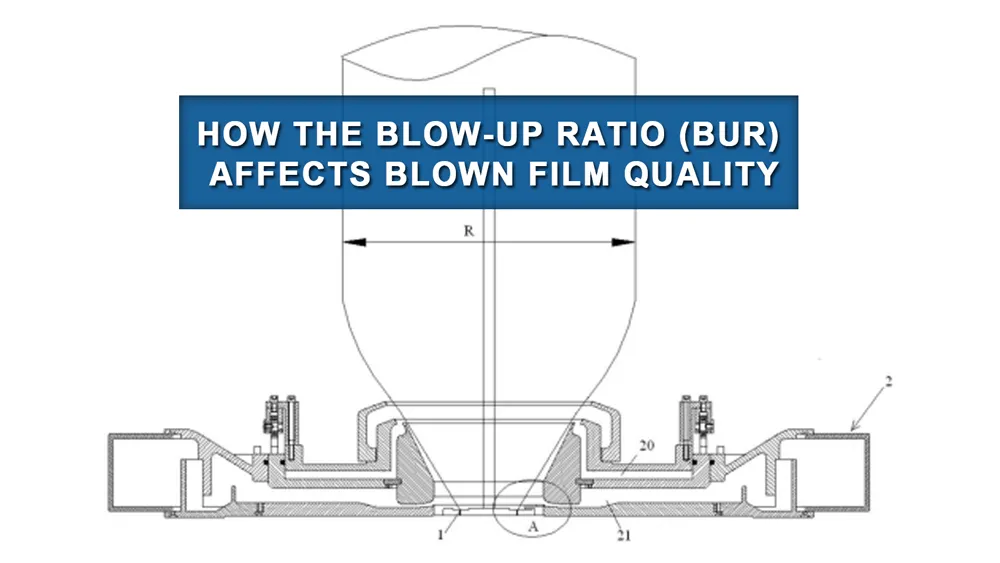
Blow-up ratio (BUR) is the ratio of the inflated film bubble diameter to the annular die diameter in blown film extrusion. It describes the transverse expansion of the film and influences film width, molecular orientation and mechanical properties.
For example, a 100 mm die producing a 471 mm lay-flat film width gives a BUR of approximately 3:1. BUR is important, but it must be evaluated together with draw-down ratio (DDR), resin and cooling conditions.
How to Calculate Blow-Up Ratio (BUR)
The bubble circumference is approximately twice the lay-flat width after the tubular film is collapsed. This gives a practical calculation using measurements available on the production floor.
Die diameter: 100 mm
Lay-flat width: 471 mm
BUR = (471 × 0.637) ÷ 100 ≈ 3.00
Result: Approximately 3:1
This formula assumes a conventional circular bubble and a lay-flat width measured without significant stretching or folding distortion. If gussets are present, use the correct developed tube circumference rather than the visible folded width alone.
How Does BUR Affect MD and TD Film Properties?
During blown film extrusion, the film is stretched in the machine direction (MD) by haul-off and in the transverse direction (TD) by bubble inflation. BUR is an important factor in this balance, but it does not determine final film strength on its own.
| Condition | General Effect | What to Verify |
|---|---|---|
| Lower BUR | Less transverse expansion relative to die diameter. | MD/TD tensile balance, tear behavior and required film width. |
| Higher BUR | More transverse expansion and potentially greater TD orientation. | Bubble stability, gauge variation, tensile balance and impact performance. |
| Excessive BUR for the Process | May increase bubble-control difficulty or exceed the stable operating window. | Bubble movement, cooling capacity and production consistency. |
Tensile strength, tear resistance and dart impact are different properties. Increasing BUR does not guarantee that all three will improve. Resin grade, DDR, frost line, cooling and film structure must also be considered.
Blow-Up Ratio vs. Draw-Down Ratio (DDR)
BUR describes transverse expansion, while draw-down ratio (DDR) is commonly used to describe longitudinal draw-down in blown film extrusion. Evaluating both provides more useful context than BUR alone.
| Parameter | What It Describes | Main Consideration |
|---|---|---|
| BUR | Bubble diameter relative to die diameter. | Transverse expansion and film width. |
| DDR | Draw-down of the extruded melt toward the final film thickness. | Longitudinal stretching and thickness reduction. |
| Frost Line Height | Position where the film visibly transitions during cooling. | Cooling conditions and film formation. |
A commonly used simplified DDR estimate is DDR ≈ Die Gap ÷ (Film Thickness × BUR), with all dimensions in consistent units. It is a process approximation, not a direct measurement of molecular orientation.
Does a Higher BUR Make Blown Film Thinner?
It can, if polymer output and haul-off conditions remain unchanged. Increasing bubble diameter distributes material over a greater film width, which can reduce average thickness. However, thickness also depends on extrusion output, line speed and process stability.
BUR alone cannot guarantee uniform gauge. If film thickness varies across the web, check die settings, cooling airflow, bubble movement and haul-off conditions before changing BUR.
How Does BUR Affect Bubble Stability?
BUR influences bubble geometry and the operating conditions needed to maintain a stable inflated tube. A ratio outside the stable process window may contribute to bubble movement, width fluctuation or inconsistent film formation.
Before adjusting BUR, check air-ring performance, cooling balance, internal bubble pressure, frost line behavior, haul-off stability and resin processing conditions. Changing bubble diameter without controlling these variables can create additional problems.
Typical Blow-Up Ratios for LDPE, LLDPE and HDPE
Different polyethylene grades have different melt strength, processing behavior and film-property requirements. The ranges below are broad starting references, not universal machine settings.
| Material | Illustrative BUR Range | Important Consideration |
|---|---|---|
| LDPE | Approximately 2:1–4:1 | Confirm melt strength, cooling and target film properties. |
| LLDPE | Approximately 2:1–4:1 | Evaluate resin grade, blends, impact and tear performance. |
| HDPE | Approximately 3:1–6:1 in some applications | Actual operating range depends strongly on grade, die and film application. |
These ranges should not replace the resin supplier's processing guidance or machine-specific trials. For a broader comparison of packaging substrates, see PP, PE and PET film materials and applications .
Blown Film Quality Problems: Is BUR the Cause?
BUR is an important troubleshooting variable, but not every blown film defect should be corrected by changing the bubble diameter.
| Production Problem | BUR Relationship | Other Checks |
|---|---|---|
| Incorrect Lay-Flat Width | Direct relationship. | Die diameter, bubble size and width measurement. |
| MD/TD Strength Imbalance | BUR can influence orientation. | DDR, resin grade, cooling and test direction. |
| Uneven Film Thickness | May contribute through bubble behavior. | Die gap, air ring, extrusion output and haul-off. |
| Bubble Instability | Operating BUR may be unsuitable. | Cooling airflow, frost line and internal bubble pressure. |
| Poor Heat Sealing | Possible indirect relationship. | Sealant material, temperature, pressure, dwell time and contamination. |
| Excessive Haze | Not controlled by BUR alone. | Resin, cooling rate, crystallization and film structure. |
How to Choose the Right BUR for Your Film
Start with the required lay-flat width, resin grade, film thickness and end-use performance. Then check whether the calculated BUR falls within the stable operating range of the die, cooling system and polymer formulation.
- Define the film: material, lay-flat width, thickness and application.
- Calculate BUR: use the actual die diameter and target lay-flat width.
- Review DDR and cooling: check the complete stretching and solidification process.
- Run controlled trials: record bubble stability, gauge profile and output.
- Test the film: verify MD/TD tensile, tear, impact and sealing performance as required.
The best BUR is not necessarily the highest or lowest achievable ratio. It is the ratio that supports the required film width and properties under stable, repeatable production conditions.
Why Blown Film Quality Matters for Printing and Packaging
Film made by blown extrusion may later be printed, laminated, slit or converted into packaging. Variations in thickness, flatness and mechanical behavior can create problems during these downstream processes.
For film printing, consistent material properties help support stable web transport and registration. Learn how substrate handling fits into the flexographic printing process .
If defects appear only after printing, distinguish substrate-related issues from ink transfer, drying and press-setting problems. Henghao's flexo printing defects troubleshooting guide covers the printing-side checks.
Blow-Up Ratio FAQ
Is BUR the Same as the Film Expansion Percentage?
No. BUR is a diameter ratio, such as 3:1. An expansion percentage describes a relative change and should not be used interchangeably without defining the calculation.
Does Lay-Flat Width Include Gussets?
For gusseted tubular film, the visible folded width may not represent half of the original tube circumference. Use the developed circumference of the tube before gusseting to calculate the corresponding bubble diameter.
Can Two Blown Film Lines Use the Same BUR and Produce Different Film Quality?
Yes. Different dies, resin grades, cooling systems, DDR settings and production conditions can produce different mechanical and optical properties even when BUR is identical.
Should BUR Be Changed While Troubleshooting a Film Defect?
Only after identifying a plausible connection to bubble width, orientation or stability. Record the baseline conditions and change one controlled variable at a time where practical.
Key Takeaway: BUR Is One Part of Film Quality Control
Blow-up ratio determines the relationship between bubble diameter and die diameter, but it does not independently determine film quality. Calculate BUR correctly, evaluate it with DDR and cooling, and verify the finished film through relevant production and laboratory tests.
For stable blown film production, the goal is not to maximize BUR. It is to achieve the required width, thickness, mechanical performance and bubble stability consistently.
Share this article: